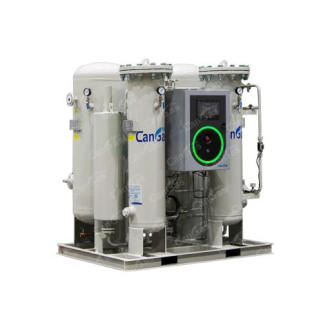
What is the PLC control sequence in a PSA nitrogen generation system
In a PSA (Pressure Swing Adsorption) nitrogen generation system, the PLC control sequence is closely linked to the process flow. Therefore, let us first review the complete PSA process, which generally consists of three steps:
1.Pressurization and Adsorption: Compressed air flows upward through the adsorption tower; the carbon molecular sieve preferentially adsorbs oxygen, carbon dioxide, and water vapor, while nitrogen flows out from the top of the tower.
2.Pressure Equalization: The tower that is nearing the end of its adsorption phase (high pressure) is connected via valves to the tower that has completed desorption (low pressure), allowing their pressures to equalize. This step significantly recovers pressure energy and reduces overall energy consumption.
3.Depressurization and Desorption/Regeneration: The pressure inside the tower is rapidly reduced to atmospheric pressure; adsorbed impurities (such as oxygen) are released from the molecular sieve and vented into the atmosphere.
Next, we will illustrate the PLC control sequence using a dual-tower (Tower A and Tower B) system as an example:
Stage 1: Tower A Pressurization/Adsorption | Tower B
Depressurization/Desorption
PLC Control Action: The PLC outputs signals to open the inlet valve and nitrogen product valve of Tower A, while simultaneously closing the corresponding valves for Tower B. This allows compressed air to enter Tower A for pressurization and adsorption.
At the same time, the PLC opens Tower B's vent valve to rapidly reduce the internal pressure to atmospheric pressure, allowing the oxygen and impurities adsorbed by the molecular sieve to be discharged, thereby successfully completing Tower B's desorption process.
Stage 2: Pressure Equalization Process
Once Tower A finishes adsorption and Tower B completes desorption, the system does not switch immediately; instead, a "pressure equalization" step is performed first.PLC Control Action: The PLC first closes Tower A's inlet valve, then opens the pressure equalization valve connecting the tops of Tower A and Tower B, allowing the pressures in both towers to balance. This conserves energy, reduces pressure fluctuations, and improves system efficiency.
Stage 3: Adsorption in Tower B | Regeneration of Tower A
Control Action: After pressure equalization concludes, the PLC closes the nitrogen product valve and pressure equalization valve of Tower A, then opens the inlet valve and nitrogen product valve of Tower B. Compressed air is diverted into the regenerated Tower B to continue nitrogen production. At this point, the PLC opens the pressure relief valve on Tower A to release pressure and purge the adsorbed impurities, thereby regenerating the molecular sieve within the tower.
Stage 4: Re‑equalization
Similar to Stage 2, a re‑equalization step is performed before the adsorption phase in Tower B concludes, preparing the system for the switch back to Tower A.
Subsequently, the PLC manages the continuous cycling of the entire process to ensure uninterrupted production.
In fact, valve control is merely a fundamental capability of the PLC; it also supports functions such as data sampling, feedback loops, and safety interlocks, enabling a system that is smarter, more automated, and safer and more stable in operation.